
Precision CNC Machining for Semiconductor Equipment
High precision components used in wafer processing, inspection, and cleanroom systems. Shenzhen XS Precision machines vacuum components, precision housings and alignment structures for semiconductor equipment builders — from a first prototype to repeat production, on the same fixture and the same programme.
A vacuum part rarely fails all at once. It fails as a pump-down that takes longer every week, as particles that turn up at the inspection step, or as a sealing face that loses its flatness the first time the chamber is baked. Most of that comes from the machining and finishing sequence rather than the design, which is why XS Precision keeps sealing geometry, coating allowance and cleaning in one place instead of spreading them across three suppliers.
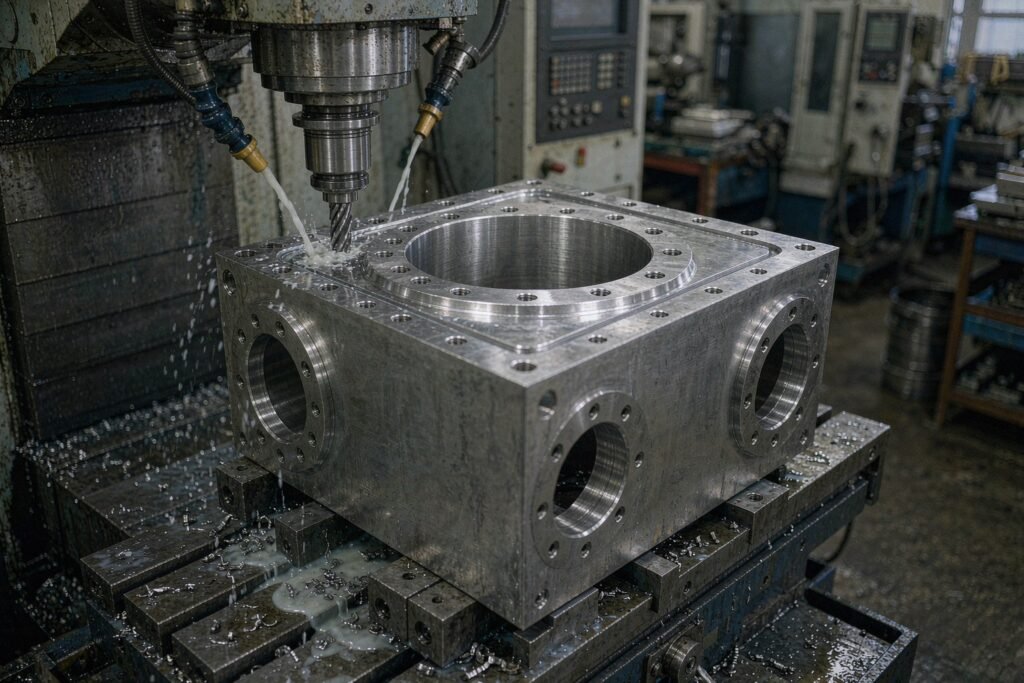
Five places in a fab where a machined part decides the result
Semiconductor work is not one job with one requirement. A showerhead plate, a load-lock door and a metrology bracket look nothing alike, and the feature that decides whether each of them works is different. XS Precision machines for all five of the positions below, and quotes them against the requirement that actually governs.
Deposition
PVD and CVD chamber liners, shields and gas distribution plates. Wall thickness and internal finish drive film uniformity and how fast the chamber reaches its base pressure.
Etch
Plasma-facing liners, edge rings and electrode housings. Any anodise or yttria layer adds real thickness, so it has to be allowed for at the drawing stage rather than found at assembly.
Lithography
Wafer stage brackets and sensor mounts, where stiffness and thermal stability matter more than a tight general tolerance. Stress relief is the control that matters here.
Metrology
Alignment structures and detector housings that hold a beam path or a camera axis where the drawing says it is, and keep it there as the tool warms up.
Vacuum transfer
Load-lock doors, slit valve seats and transfer chamber covers, where the flatness of a sealing land sets the leak rate and the pump-down time for everything upstream.
One supplier from billet to sealed bag
Splitting a chamber part across a machinist, a coater and a cleaning house is normal practice and it is also where most of the trouble starts. Each hand-off adds a fixture, a transport and a set of assumptions about who owns the finished dimension.
Sealing geometry cut in one set-up
A chamber face, the O-ring groove around it and the bolt-hole circle that closes it are machined without releasing the part. Re-clamping between operations is what turns a sealing land into a leak path.
Coating allowance planned into the drawing
Hard anodise, a conversion coating or a thermal spray layer all take up space. Bore and groove dimensions are issued for the finished part, and the pre-coat size is the one we machine to.
Stress taken out before the finishing cut
Rough machining, stress relief, then finishing. Parts that are cut to size in one pass move when the chamber is baked, and the flatness number on the drawing stops being true.
Cleaned, tested and packed on the same site
Ultrasonic cleaning, DI rinse, leak testing and cleanroom bagging all happen in Shenzhen before the part travels, so nothing has to be re-cleaned after being shipped across the country.
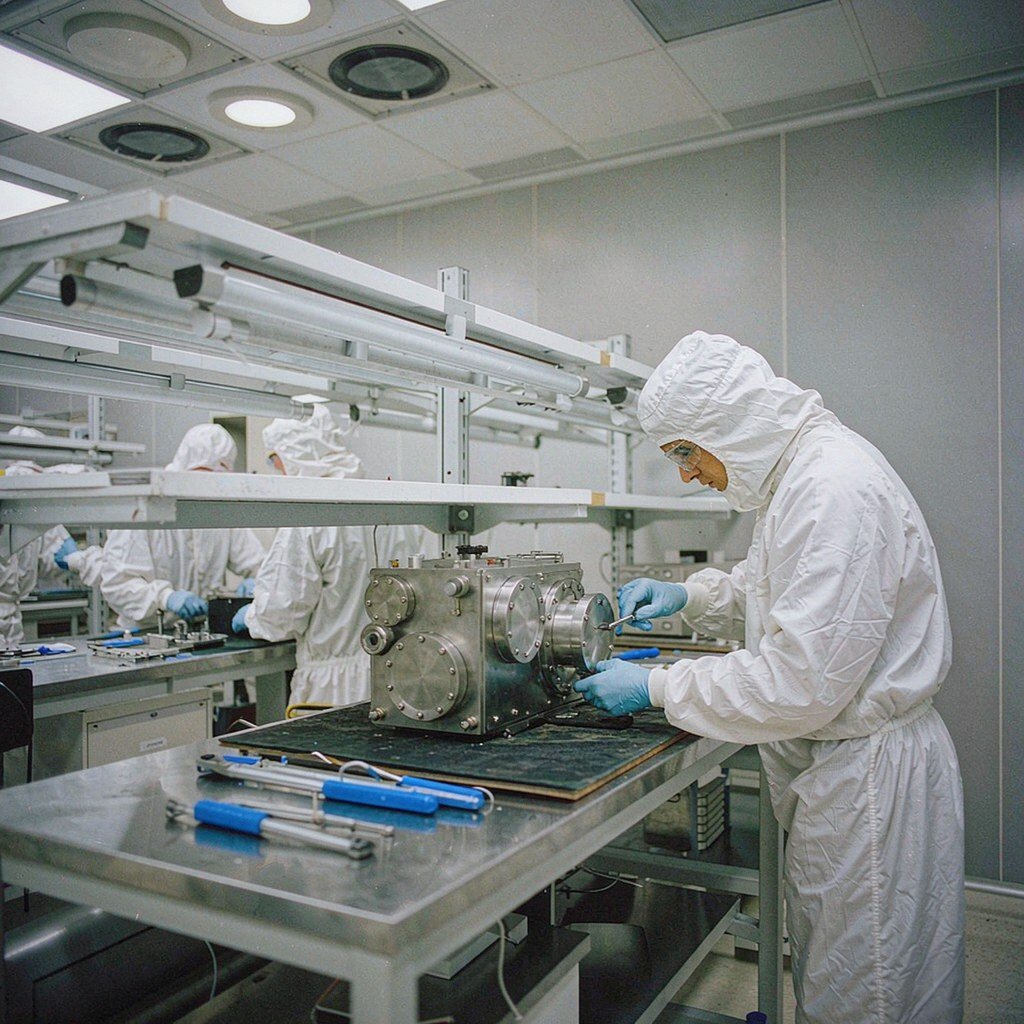
Three part families we machine for wafer tools
High precision components used in wafer processing, inspection, and cleanroom systems. Three families make up most of the semiconductor work XS Precision runs for tool builders and fab maintenance teams:
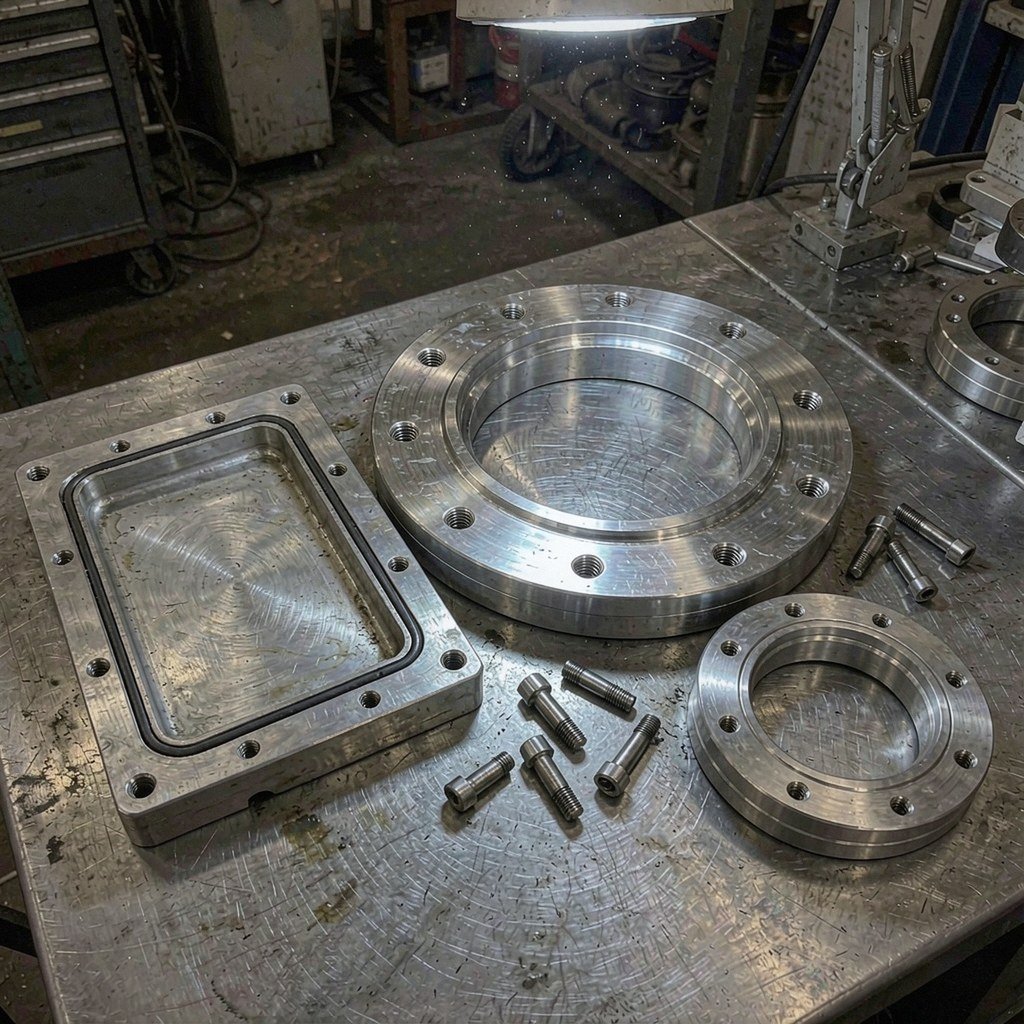
Vacuum components
- Chamber bodies, lids, port flanges and sealing plates
- CF knife-edge profiles, KF seats and O-ring grooves
- Blind tapped holes vented so they cannot hold a virtual leak
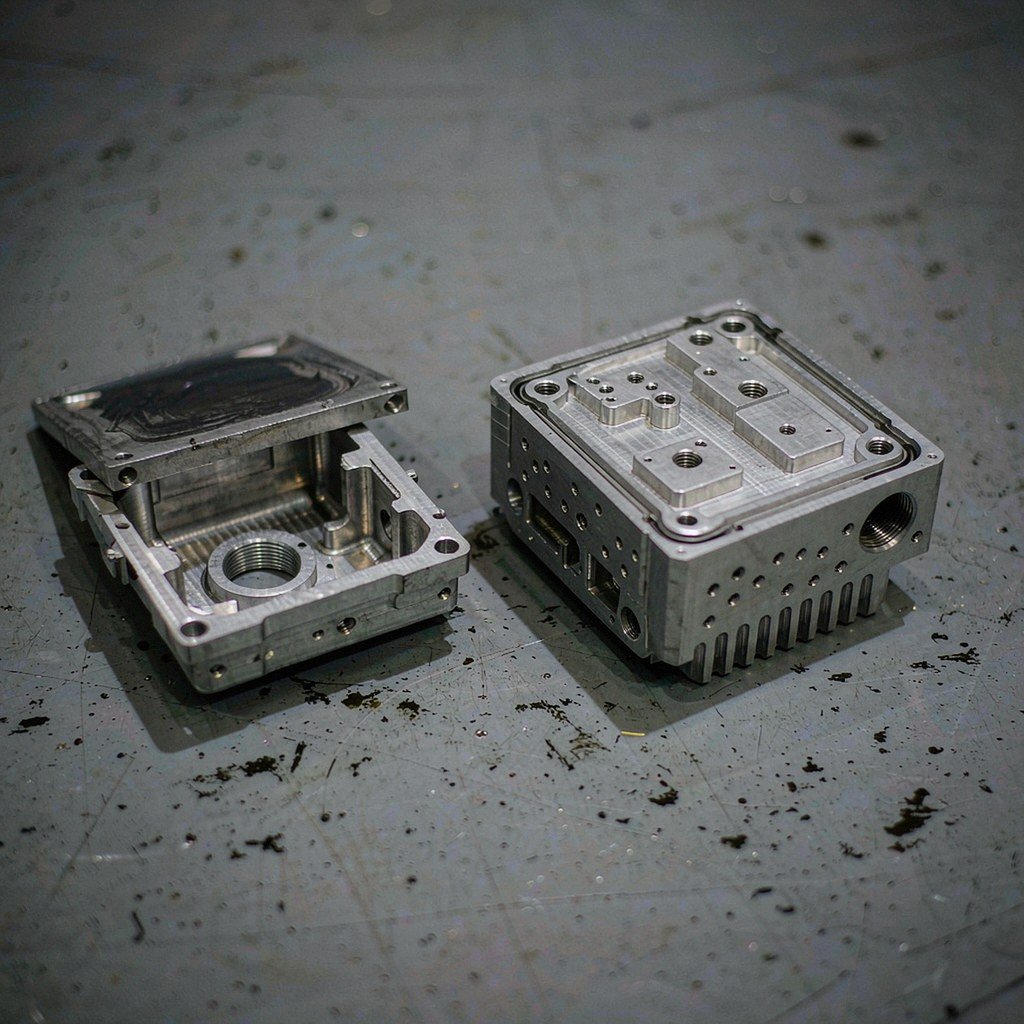
Precision housings
- Sealed enclosures for detectors, sensors and drive electronics
- Gasket grooves, EMI lands and connector cut-outs
- Wall thickness controlled for stiffness, weight and heat path
Alignment structures
- Base plates, brackets and frames with interface datums
- Kinematic seats, dowel holes and fine-pitch adjusters
- Flatness and hole position tied to the assembly datum chain
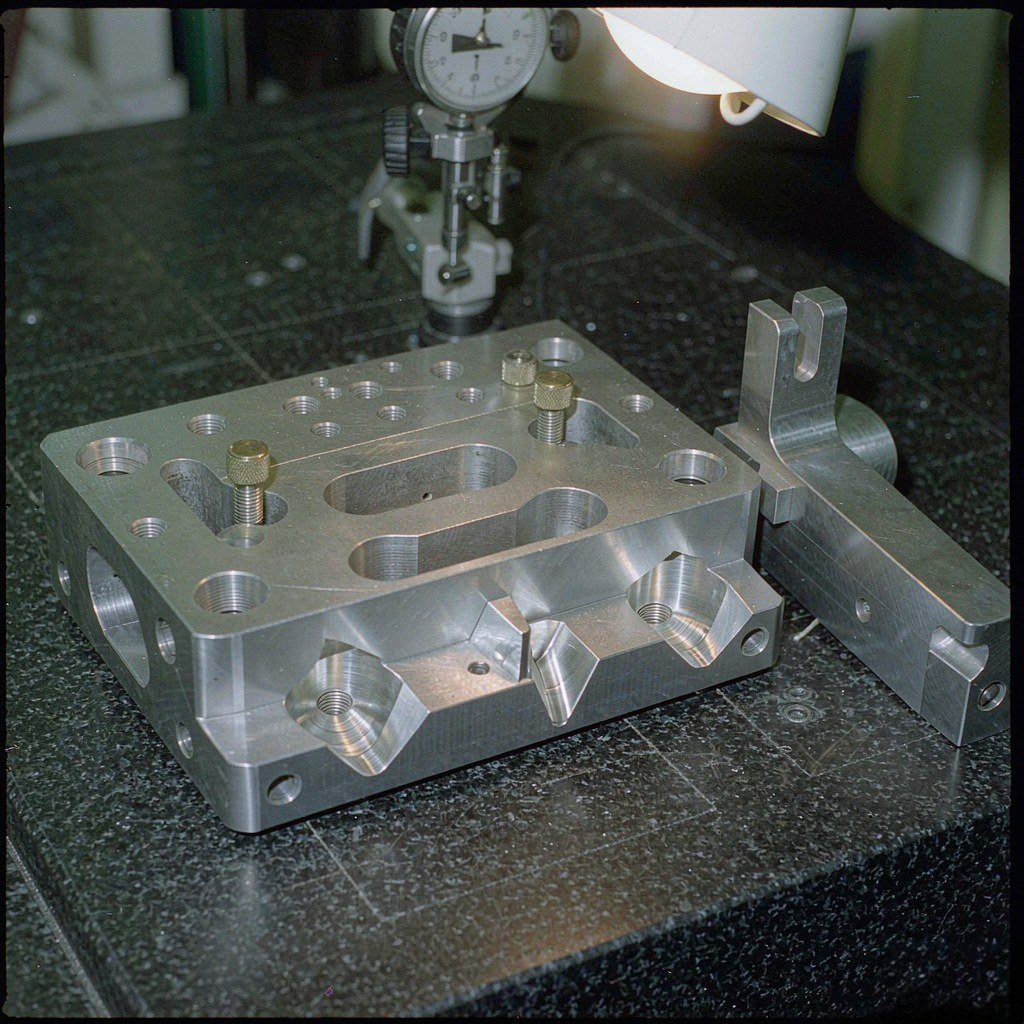
Six ways a machined part costs a wafer batch
These are the six problems that come up again and again when a machined part goes onto a semiconductor tool. None of them shows up on a general dimensional report, which is why XS Precision tests and documents the specific thing that fails in each case.
A tapped hole that bottoms out with nowhere for the air to go will bleed into the chamber for hours. Every blind hole on a vacuum-facing part here gets a vent slot or a through hole, so pump-down behaves the same on part one and on part two hundred.
Overall size can pass inspection and the face can still rock. Flatness and surface finish on the sealing land are measured and reported separately, at the temperature the drawing names rather than the temperature of the shop that afternoon.
Hard anodise, chromate conversion and yttria spray add anywhere from 25 to 200 µm. If the pre-coat size is not planned against the finished part, the groove comes back undersize from the coater and the whole batch is rework.
A CF knife edge seals on a narrow ridge. Chatter or one nicked edge there will not hold, however good the rest of the part is, so those profiles are finished with dedicated tooling and checked under magnification before the part moves on.
Burrs, abrasive media and cutting fluid residue all release particles and organics once they are under vacuum. No abrasive blasting on sealing surfaces, ultrasonic and DI rinse, then bagging before the part leaves the building.
A fab needs a heat lot, a certificate and an inspection record before it can accept a part. Material certificates, CMM reports and leak test logs are issued with the shipment as standard, not chased up afterwards.
Capability, stated as numbers
These are the working limits XS Precision quotes on semiconductor work. Where a drawing asks for more than this, the honest answer is a different process rather than a different promise.
Chosen for what the chamber does to them
Material call-outs on semiconductor drawings are not taste. They follow the chemistry inside the chamber, the temperature it runs at and what the part is allowed to release. XS Precision works to the customer’s list and says so early when a grade is going to fight the process.
Aluminium
Chamber bodies, liners, carriers and cold plates. Easy to hold to close tolerance and quick to pull heat away from a wafer, which is why most PVD and CVD hardware is aluminium. See the aluminium machining notes for how anodise thickness is planned into a bore.
Stainless
Plasma-facing liners, gate valve parts, welded gas channels and anything that sees halogen chemistry. Low-sulphur 316L machines to a finer finish, and electropolishing takes the internal surface down to Ra 0.2 µm, which lowers both outgassing and the area that can hold residue.
Polymers and titanium
Insulating spacers, seal supports, end effectors and RF parts. Vacuum-grade stock is used rather than general-purpose, and bake-out data is available: a 24-hour bake at 200 °C should stay under 1 % total mass loss before a polymer goes inside a chamber.
Contamination control starts at the material call, not at the cleaning tank. Copper and zinc-bearing alloys stay out of process-facing parts unless the customer’s own specification asks for them, and every polymer that goes inside a chamber arrives with a lot number and a data sheet.
How an order runs
Rough and stabilise
Bulk material comes off first, then the part is stress relieved before anything is finished. On a large chamber face this step is what keeps the flatness number true after the first bake cycle.
Finish in few set-ups
Five-axis work keeps the sealing land, the groove and the bolt pattern on one datum. Features that cannot be reached in a single set-up go onto a dedicated fixture rather than being blended by hand.
Measure, then test
CMM reports cover dimensions and position; sealed assemblies get a helium leak test; surface finish is measured on the sealing faces. The numbers go into the file that travels with the part.
Clean and pack
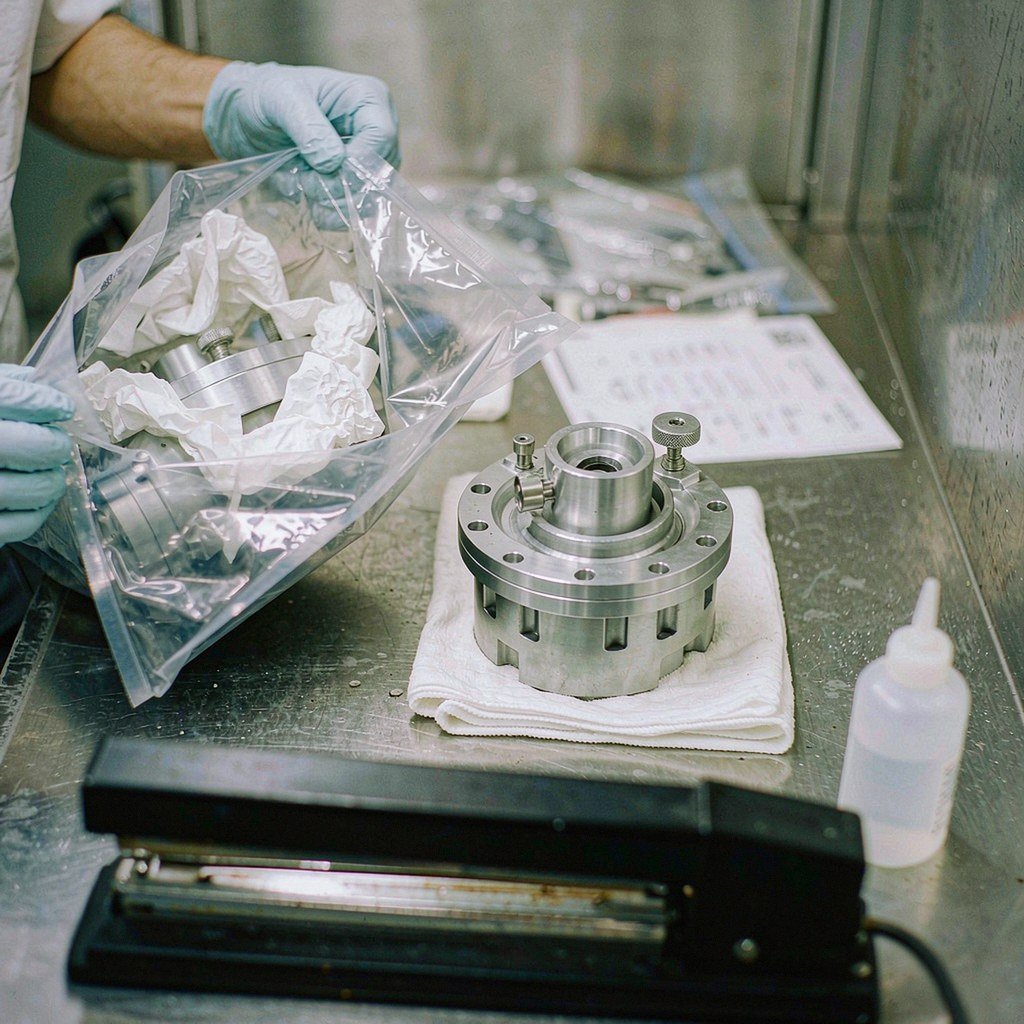
Ultrasonic clean, DI rinse, dry, then double-bagged in the cleanroom with the certificate inside the outer bag. The part arrives ready to install rather than ready to re-clean.
Every part leaves with evidence

The paperwork is not an afterthought bolted onto the end of a job. It is the reason a semiconductor customer can put a Shenzhen-made part into an approved-vendor file, and the reason a fab can accept a second-source part without opening a fresh qualification cycle.
Heat number, grade and chemistry on file for the billet each part was cut from, to EN 10204 3.1 where the customer asks for it.
Sealing dimensions, groove geometry and knife-edge profiles are verified while the part is still on the machine, not after it comes off it.
First article and sampling reports against the drawing, covering dimensions, true position, flatness and any datum the drawing names.
Helium test result, the instrument used and the acceptance limit, recorded per sealed assembly rather than per batch.
Cleaning sequence, bag material and the date the part was sealed, so an incoming inspection can be closed out against something.
What engineers ask before sending a drawing
What tolerance can you hold on a vacuum chamber body?
±0.010 mm on machined features and 0.005 mm flatness per 100 mm on sealing lands and datum faces. On a large part that is a process limit rather than a promise: the fixture, the stress relief sequence and the temperature of the room all have to be right before the number means anything.
How do you stop virtual leaks?
Every blind tapped hole on a vacuum-facing part gets a vent slot or a through hole so trapped air has somewhere to go. It costs a few seconds of machine time and it is the difference between a chamber that pumps down in hours and one that keeps creeping for a week.
Do you arrange anodising and plasma-spray coatings?
Anodising, hard anodising, chromate conversion, electropolishing and passivation are handled with finishers we work with regularly, and yttria or alumina thermal spray on plasma-facing parts is arranged the same way. The pre-coat dimensions are ours to plan, and the part is re-measured after coating before it is accepted.
Can you hold a helium leak rate specification?
On sealed assemblies we test to 1×10⁻⁹ Pa·m³/s with helium mass spectrometry and log the result. Parts that do not meet it are reworked or scrapped here rather than shipped with a note attached.
What does cleanroom packaging actually mean here?
Parts are finally cleaned, dried and bagged in a controlled area, then double-bagged for shipment with the paperwork inside the outer bag. If your incoming inspection expects a named bag material, a nitrogen purge or a particle count, put it on the drawing and it will be followed.
Can you take on a second-source qualification?
Yes, and that is most of the semiconductor work we do. Send the original drawing and, where you have them, the OEM inspection report and the material call-outs. The first order is normally a small batch run against the same inspection plan, so your engineering team can compare the paperwork before volume starts. Drawings, tooling and process details stay with the customer under NDA.
Where to go next
Precision CNC machining
Machine set-ups, tolerance capability and the 5-axis process behind these semiconductor parts.
Material expertise
Aluminium, stainless, titanium and engineering plastics, and what each one does under vacuum.
High-precision components
Where the tightest tolerances sit, and what has to be settled with us before a process is fixed.
Send the drawing. Get a manufacturability answer back.
A STEP file, a material call-out and a leak-rate target are enough to start. Shenzhen XS Precision returns a price, a lead time and a note on any feature that will be expensive to hold — before the first part is cut. NDA and drawing control are standard, and nothing made for one customer is shown to another.