
Low Volume Production for 1 to 5,000 parts
There is no tooling bill on this page. Every part below is cut from billet on the same machines that run our larger orders, so the question is never whether the part is real — it is only how the fixed cost spreads. That single number, not the hourly rate, decides what your unit price looks like. XS Precision runs low volume production from one piece to a few thousand a year, quotes every job at five quantity breaks, and tells you when the batch size on your purchase order is the expensive one.
Six numbers that decide a low volume quote
Before any cycle time is calculated, these six figures have already set the shape of the price. Four of them come from the batch size alone.
The cost curve is a fixed-cost story, not an hourly-rate story
A 6061-T6 bracket with two setups and ordinary tolerances is a good test case. The machine rate does not change between one piece and a thousand. What changes is how many parts get to carry the programming, the fixture and the first-article verification. On a single part those fixed items are most of the invoice. On a thousand they are a rounding error, and material and cycle time take over.
The solid bar below is the fixed share. The hatched bar is everything that scales with the piece. Watch the fixed share collapse between the first and the third row — that is the whole reason a small batch behaves so differently from a single part.
Read the last two rows together and the practical rule falls out. Going from one piece to ten cuts the unit price by roughly two thirds. Going from 100 to 1,000 saves around 13 percent. Going from 1,000 to 10,000 saves about eight. If a supplier only gives you one quantity, you cannot see any of this — which is why XS Precision quotes the same job at 1, 10, 50, 200 and 1,000 pieces on every RFQ.
What actually changes at each quantity tier
The quantity breaks are not arbitrary round numbers. Each one is the point where a different strategy becomes the cheap one, so each one changes what the shop should be doing with your part on a Low Volume Production order.
- Standard vise fixturing keeps overhead out of the price
- Ask for the parts to be machined on the production machine, not a separate sample setup — a first article from a different machine is not a valid production first article
- Chase design changes now; every revision after this point costs a fixture and a re-qualification
- Soft jaws milled to the part profile replace the vise
- A ten to fifteen working day window is normal
- Batch the order. Two orders of ten are not the same thing as one order of twenty
- Multi-part fixturing holds four to eight parts per cycle
- In-process checks on critical dimensions become routine
- Ask for the fixture to be kept — the next order runs cheaper
- Multi-part fixtures plus lights-out running change the economics
- Material cost is now a large share of the unit price, so the blank strategy is worth an argument
- Request the comparison: machining versus tooling, side by side
- Soft tooling in aluminium runs 500 to 10,000 shots
- Shared mold bases with custom inserts cut tooling cost by 50 to 70 percent against a full hardened tool
- bridge tooling buys time and validates material without committing to a hardened mold
Workholding is where the setup cost actually goes
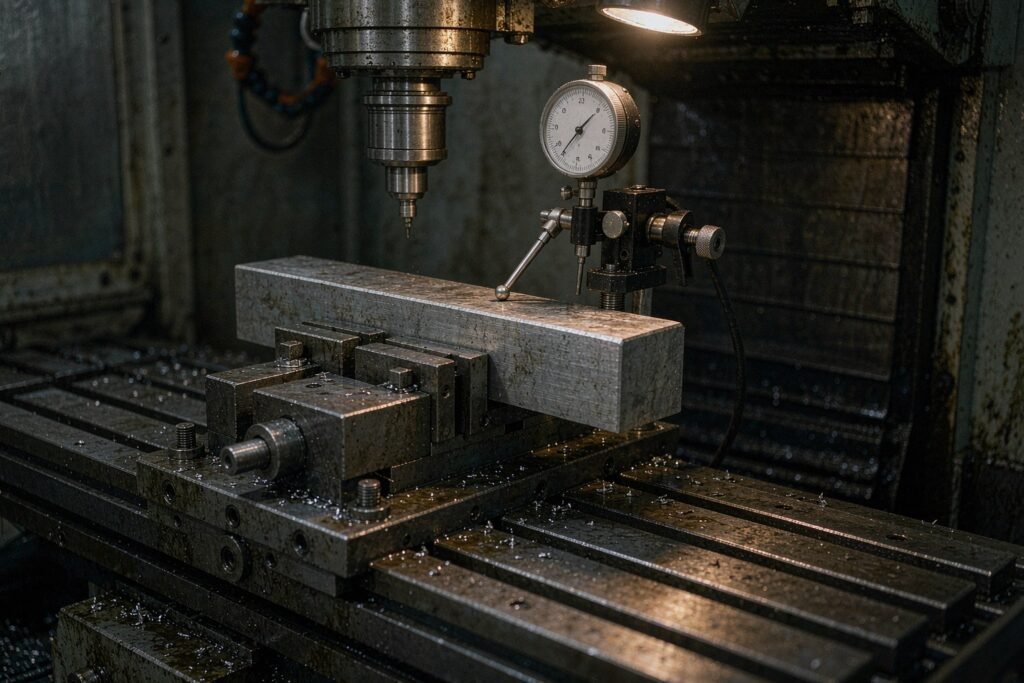
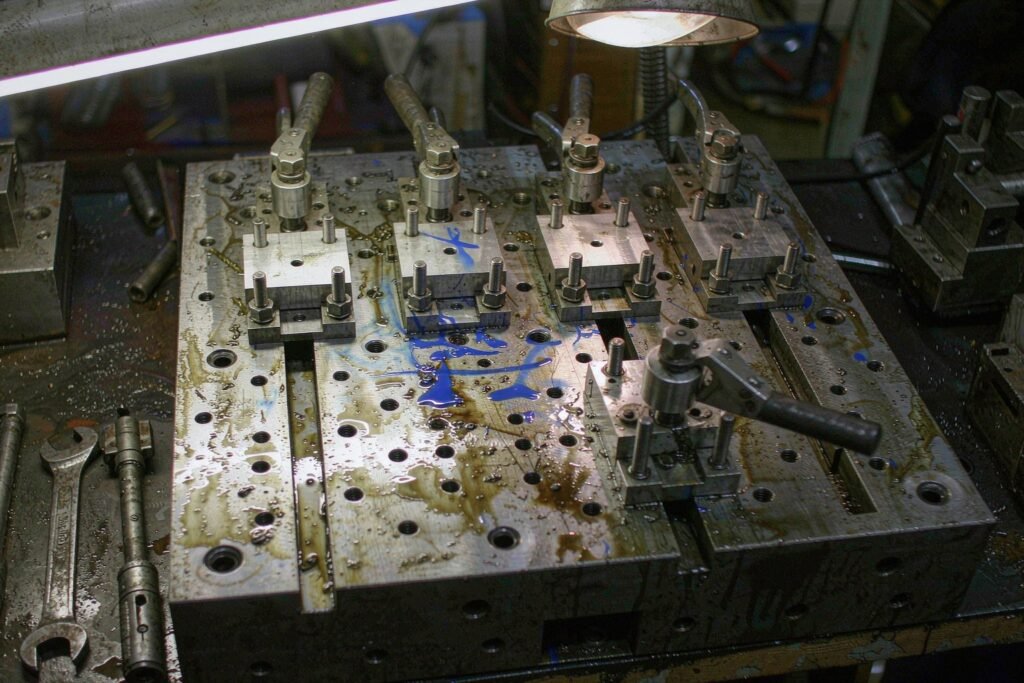
The first-piece setup and the multi-station fixture below are the two ends of the same decision. On ten parts the setup is a vise and a dial indicator. On three hundred the setup becomes a plate that holds several parts at once, and the time saved per cycle is what pays for it.
Splitting one order into two is where the money goes
A published case makes the point better than any model. A team ordered ten prototype housings at $74 each. Two weeks later they needed twenty more and placed a second order for twenty, at $68 each. A single order of thirty would have come in at $52 per part. The parts were identical, the drawing was identical, the machine was identical. The only thing that changed was that the setup had to happen twice, and the fixed cost was paid twice on a batch that was never big enough to absorb it.
The arithmetic on that job is about $480 of avoidable cost. Most low volume programs lose that amount repeatedly, not once, because internal prototype requests are approved one at a time. The fix costs nothing: collect the requests and release them as a single purchase order with quantity breaks already agreed with the supplier.
Tolerance is the second multiplier, and it is easy to overspecify
Most drawings arrive with every dimension at one tight figure, usually ±0.025 mm or tighter, when the part would work at the ISO 2768-medium default. The multipliers below are measured against that default, and they compound with the batch size: an overspecified part at low quantity is expensive twice over.
The right move is to put one general class in the title block — ISO 2768-mK is the safe default for machined parts — and then apply a tighter number only to the features that genuinely need it: a bearing seat, a sealing face, an indexing dimension, a mating edge. A part with two tight features and everything else at the default stays close to baseline cost. The same part with the tight number applied globally is a different job entirely.
Surface finish follows the same logic. Taking a face from Ra 3.2 to Ra 0.8 can push the finishing cost up by 200 to 400 percent, because it needs an extra pass, a different tool, or a trip to the grinder. Specify roughness only where a surface actually functions as a seal, a bearing seat or a sliding face.
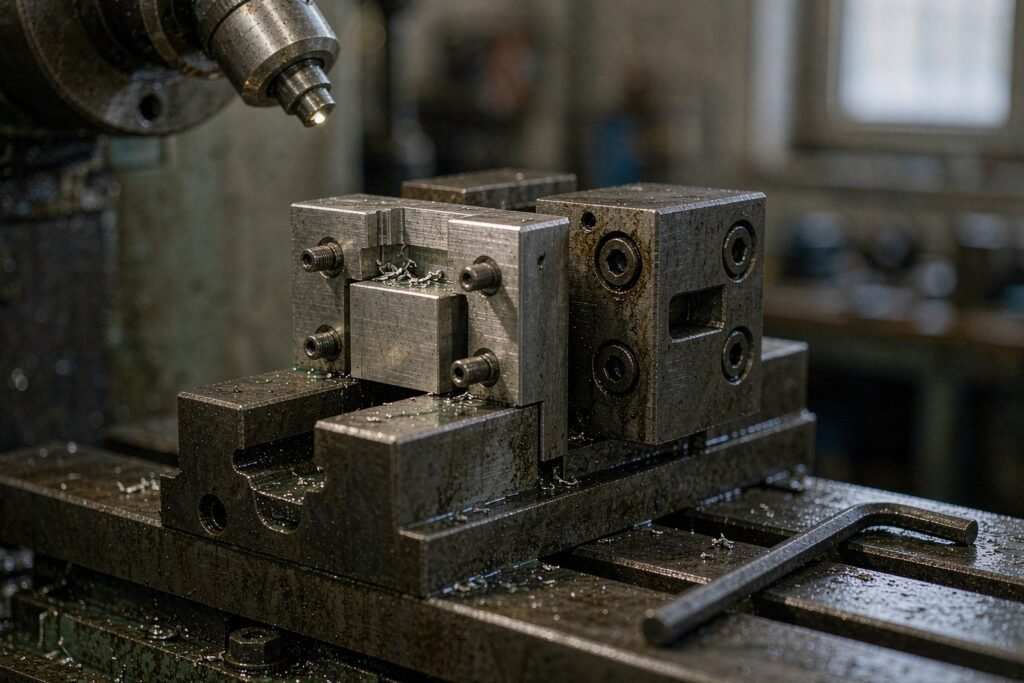
Soft jaws milled to the part profile in a standard vise, the part located on dowel pins. On a small batch this is usually all the workholding a part needs, and it costs nothing beyond the machining time.
One more thing that catches people out: the multiplier applies to the process, not to the feature. Adding a single ±0.02 mm note to one critical width costs far less than tightening the general class across a drawing with forty untoleranced dimensions on it, because the general class touches every one of them. That review is part of every quote XS Precision issues.
First article inspection costs the same on 10 parts as on 500
A first article inspection is not a spot check. Every dimension on the drawing is measured and reported with an actual value, and for regulated programs that means an AS9102 package: part accountability, characteristic-by-characteristic results, and material and special process certificates. The measurement work is the same whether the order is ten pieces or five hundred, so the per-part cost grows as the batch shrinks.
That is why aerospace and medical quotes look so different from commercial ones at low quantity. A commercial quote has no first article line at all. A regulated quote carries a line item that can run from a few hundred to a few thousand dollars, and on a ten-piece order it dominates the invoice.
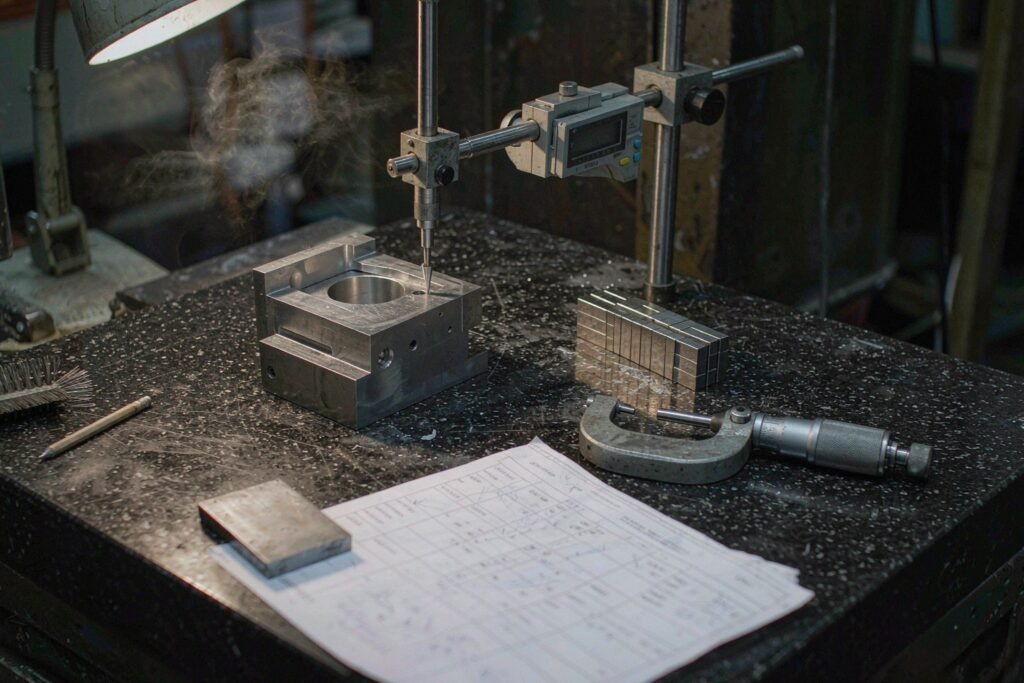
Three things reduce the bill without skipping anything. First, a delta first article: when a revision changes only some features, re-measure those and reference the previous report for the rest, provided that report is still valid. Second, measure once and let the CMM output feed the report template directly instead of retyping values. Third, and most useful at low volume, keep the part number in production. A first article is triggered by a new part number, a process change such as a new machine, fixture, program or material source, a design change, or a long gap in production — commonly 12 or 24 months. A program that orders twice a year keeps re-qualifying; one that orders steadily does not. XS Precision flags the dormancy rule before the first order rather than after.
Four events that put you back in the first-article queue
None of these are optional on a program that flows down the requirement, and none of them depend on the parts looking identical. The first article approves the process, not the geometry.
| GATE 01 New part number | A full first article is required on the first production run, and it must be run on the production machine with the production fixture and toolpath. | Form 1 part accountability Form 2 characteristics Form 3 material and processes |
| GATE 02 Process change | Moving the job between machines, re-fixturing it, re-programming it or changing the material source is a change of process, so the previous approval no longer covers it. | New machine or fixture New toolpath New material supplier |
| GATE 03 Design change | A drawing revision with dimensional changes requires at least a partial first article. Whether it can be partial depends on what actually changed and on the customer accepting a delta submission. | Delta report for changed features Reference to the prior report Revision letter recorded |
| GATE 04 Production gap | Many programs specify a dormancy period, commonly 12 or 24 months, after which a part that has not been run must be re-qualified even if nothing about it changed. | Dormancy period stated on the PO Re-run of first article Fixture and program re-verified |
Two of these are worth designing around. If you know a part will be ordered in bursts, ask what the dormancy rule is before the first order, because the answer decides whether a stock buffer is cheaper than a second qualification. And if a program requires a full automotive-style submission with an initial process capability study, note that the common requirement is a 30-piece study for the capability data. A twenty-piece order cannot produce that study, so either the batch gets raised to thirty or the capability requirement has to be agreed differently up front.
Thirty parts a year is not enough data for a classic control chart
Standard control chart theory was built for runs that lasted weeks. In a high-mix, low-volume shop the entire production run can be smaller than the number of points needed to calculate control limits, so the chart ends before it says anything. The answer is not to skip statistics. It is to change what gets plotted, so the parts share the work of building the limits.
Two rules keep this honest. The grouping has to be real — same machine, same process route, same material, same gauge, similar tolerance widths. Grouping unrelated jobs onto one chart is the most common reason low volume statistical process control fails, because the limits then describe nothing. And for a short run, it is normal to widen the assumed process spread and to set a higher capability target than the textbook figure used for long production runs, precisely because there is less data to prove the process with. XS Precision groups a family before it charts it, and says so when the family is not real.
Where machining stops and tooling starts
The crossover point is asked about on almost every low volume project, and the honest answer is that it is lower than most teams expect for simple geometry and much higher for complex or still-changing parts. What makes the decision easier is that there is now a middle step: tooling that is cheap and fast enough to commit to before the design is frozen.
Lead time moves before price does
In 2026 the more reliable early signal of a tight machine shop market is not a price increase, it is quoted lead times drifting on several suppliers at once. Raising a price risks losing the customer outright; quoting a longer turnaround is simply an honest statement about the backlog. So when four shops that quoted a week last quarter all quote three to four weeks now, that is capacity tightening, and it is visible well before it shows up in published market data.
The other change is what buyers are counting. Total landed cost rather than unit price is driving a reported 79 percent of US manufacturers to move sourcing decisions back toward domestic supply, and a large part of that arithmetic is the cost of handoffs. Every time a part moves to a different vendor it picks up freight, queue time, another quoting cycle and another chance for a tolerance to drift. A supplier that can turn, mill, finish and inspect without shipping the part across town four times removes cost that never appears on any single invoice. XS Precision turns, mills, finishes and inspects in one place for exactly that reason.
| GATE 01 Lead times lengthen across several suppliers at once | Capacity is tightening. This is the moment to lock a slot rather than to negotiate on unit price, because the price will hold longer than the schedule will. | Ask for a booked slot Confirm the raw material item Agree an inspection date, not just a ship date |
| GATE 02 A part needs four different vendors to finish | Every handoff adds freight, queue time, a re-quote and a fresh opportunity for a datum to be misread or a revision to get lost. | Consolidate turning, milling, finishing and inspection One traveller, one revision, one inspection report |
| GATE 03 Volume is stable but the design is not frozen | A blanket order locks raw material pricing and reserves machine capacity while leaving the release schedule open, so you are not guessing the final quantity in advance. | Blanket order with scheduled releases Fixed price, open dates Material bought against the blanket, not the release |
| GATE 04 The part has been bought at one quantity for two years | Prices at a single quantity hide the curve. A different batch size is usually a bigger lever than a different supplier. | Quote at five breaks Compare landed cost, not unit price Check whether two annual orders should be one |
Revision control is what keeps a 200-part run worth having
A low volume run is short enough that a single revision slip can consume the whole batch. The failure is rarely dramatic: a drawing revision issued after the first parts were cut, a program that still carries the previous tolerance, a fixture built to the old datum. By the time anyone notices, half the batch is scrap and there is no time to re-cut it before the delivery date.
The protection is unglamorous and it works. Freeze the drawing revision for the duration of the run, record which revision the program and the fixture were made to, and require an explicit written authorisation before anything changes mid-run. When a revision does have to land, the question to ask is not how to make it fit but whether the current batch should be completed to the old revision and the new one started clean. On a 200-part order that is usually the cheaper answer even though it feels slower.
- The assembly drawing, the part drawing and the bill of materials are all at the same revision letter before the first chip is cut
- The CAM program carries the revision it was built from, and the fixture carries the datum it was made to
- Every revision issued mid-run has a written authorisation that states whether the current batch finishes to the old revision or is scrapped
- The traveller records the revision, the machine, the material heat or lot and the operator for the actual parts that shipped, not for the batch plan
- Any dimension that changed between revisions gets re-measured on the first part of the new revision, even if the change looks cosmetic
- Rejected parts are physically separated from the good ones, because a mixed bin is how a low volume batch fails at the customer
When there is no drawing left, the part is the drawing
Some of the most useful low volume work is replacement rather than new production: a valve internal, a pump shaft, a gearbox component, a bracket for a machine whose maker stopped supporting it a decade ago. The original drawing is gone. The OEM lead time, if the part is available at all, is measured in months and the machine it belongs to is losing money every day it stands still. This is Low Volume Production at its most useful.
A physical sample is enough to work from. XS Precision measures the worn part, work the original geometry back from the wear pattern, build a model, and machine a direct-fit replacement. Where the sample is broken or incomplete, the mating component tells the missing half of the story, so send that too if you have it. Typical turnaround for a straightforward part is under two working weeks, before heat treatment or coating.
The step that actually saves money is the one people skip: archive the model. Once the geometry is captured, the next requirement is a re-machining job, not another reverse engineering job. The measuring and modelling effort gets paid for once and used for the life of the equipment. While the geometry is being rebuilt it is also worth asking whether the original material was the best available choice — a bronze bushing that wears too fast, or mild steel that should have been through-hardened, can usually be improved without touching a single mating dimension.
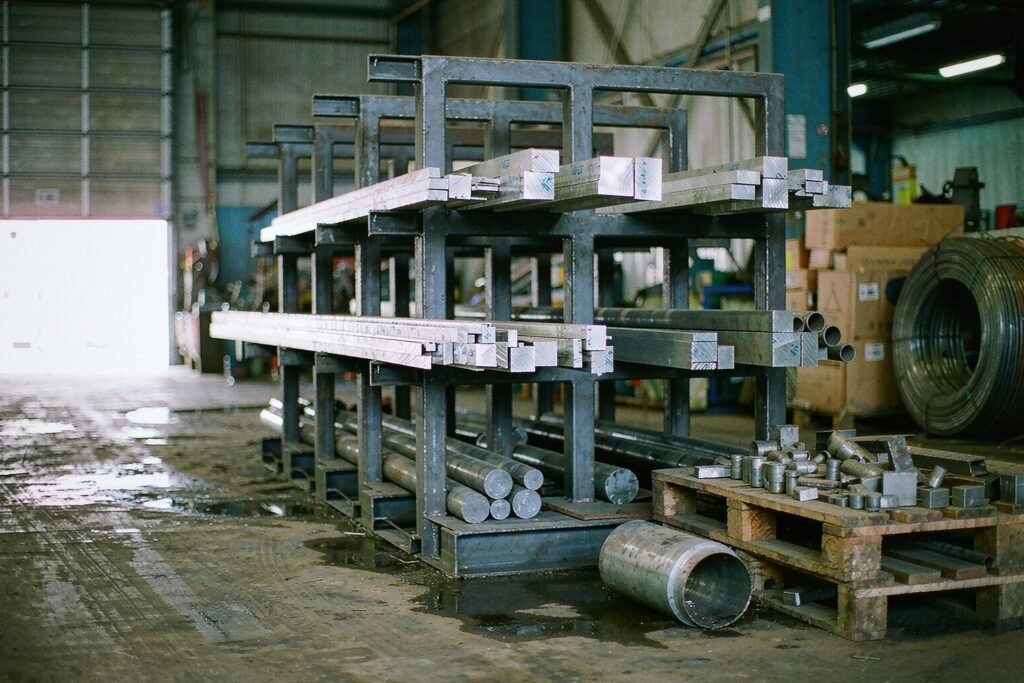
Bar stock on the rack and the offcuts below it. On a low volume order the blank you buy is a real line in the price, so the cut length and the stock size are worth an argument before the drawing is released.
- Send the worn part even if it is broken in two — a fracture face still carries the original geometry
- Send the mating component as well when fit is the open question
- Photographs straight onto each face with a caliper or tape visible across the critical dimensions work when nothing can be shipped
- State the fit, not just the size: press into a given bore, slide on a given shaft, locate against a given datum
- Mention the service conditions and the age of the machine so material can be chosen for the application rather than copied by default
- Ask for the CAD model to be archived against your account, so the next order is a re-machine
Questions we get asked before a low volume run
These are the questions that decide whether a small batch comes in on budget. Some of the answers cost us the job, which is the point.
What is the smallest quantity you will run?
One piece. There is no tooling to amortise on a machined part, so a single unit is a legitimate order rather than a favour. It will be the most expensive part you ever buy from us, and the quote will show exactly why: programming, fixture setup and first-article verification all land on that one piece. If one part is what you need, order one part.
Why is 10 pieces almost as expensive as 50?
Because the fixed cost is the same. Programming, workholding and the first-piece check are charged once per run regardless of how many parts come out of it, and on ten pieces those items are still most of the price. By fifty they have spread far enough to stop dominating. The step from ten to fifty usually moves the unit price far more than any negotiation will.
Should I place one order or two?
One, unless there is a real reason not to. Two orders of ten cost more than one order of twenty because the setup is paid twice, and the second batch also queues behind other work. If you are unsure of the final quantity, place the larger order and take delivery in two releases — that keeps the setup cost down without holding all the parts at once.
Do I need a first article inspection on a small batch?
Only if your contract asks for it. On commercial industrial work there is usually no formal requirement, and a dimensional report on the critical features is enough. If your program flows down an aerospace or automotive requirement, the first article is not optional and it will be the largest single line on a small order. Tell us it applies before we quote so it is in the price rather than a surprise.
How do you control quality when the batch is too small to chart?
By plotting the process rather than the part. Similar jobs that share a machine, a process route, a material and a gauge are grouped into a family, and the measurements are converted so they can share one chart — either as deviations from nominal or as standardised values. Fifteen different parts can then build one set of limits between them. Grouping is the part that has to be honest; if the family is not real, the limits mean nothing.
At what quantity should I switch to tooling?
It depends far more on the part than on the number, which is why we quote both rather than answer with a rule. Complex geometry, tight tolerances and a design that still moves all keep machining cheaper for longer. Simple geometry in a frozen design can justify an aluminium tool well below the volume most people expect. The useful question is not where the crossover is in general but where it is for this part, and that is a five-minute calculation once we have the drawing and the annual quantity.
Where this fits with the rest of the shop
Tell us the part and the quantity. We will quote it at every break.
Send the drawing or the 3D model, the material, and the batch sizes you are considering — even if you have not chosen one. The quote for your Low Volume Production program will show the same part at 1, 10, 50, 200 and 1,000 pieces so you can see where the curve flattens before you commit. If the batch size on your order is the expensive one, we will say so.