
Machined Carbon Steel and Alloy Steel Parts for Load-Bearing Work
Carbon Steel is what most mechanical structures are actually made of, and C45 is the grade that carries the load. XS Precision machines both sides of that choice — plain carbon steel where the section is thin enough to harden through, Alloy steel such as 42CrMo4 where it is not.
The properties that put steel on the drawing are High strength, a Cost-effective bar price and Good machinability in the annealed and normalised conditions. The property that decides whether you get all three is hardenability, and that is a question about diameter, not about the grade name.
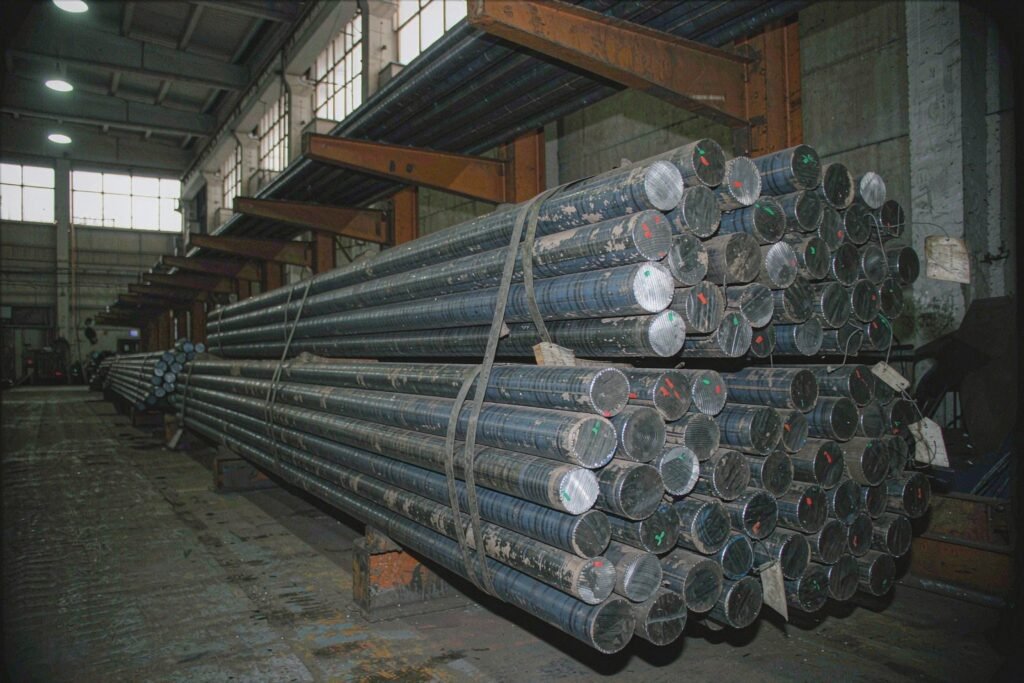
Hot-rolled carbon steel bar, sawn and tagged before it reaches a machine
C45 carbon steel: the six numbers that decide the drawing
C45 (EN 1.0503, AISI/SAE 1045, JIS S45C, GB 45#) is a medium-carbon structural steel with nominally 0.45% carbon. Mills routinely dual-certify the same heat to all four standards, so the grade names are interchangeable in practice. What is not interchangeable is the section size.
Good machinability is a property of the heat treatment, not the grade
The handbooks quote one machinability number for C45. The shop sees three, because the same bar behaves differently depending on what the mill or the heat treater did to it before it arrived.
Soft annealed C45 at 160–190 HB is the easiest thing on this page to cut: the chips break, the cutting forces are low, and the surface finish comes out clean in one pass. Normalised C45 at 170–220 HB is a little tougher because the pearlite is finer, but it is still routine on carbide. Quenched and tempered C45 is the one that changes the plan — from roughly 250 HB upward, tool wear and cutting forces both climb, and the feed and speed have to come down to protect the tolerance you are trying to hold.
Turning speeds that work on C45
With coated carbide in the normalised or annealed condition: turning 240–330 m/min, milling 150–205 m/min, parting off 115–155 m/min, grooving 135–185 m/min, drilling 95–130 m/min. In the quenched and tempered state, drop the turning speed by roughly a third and expect to spend tool life instead of cycle time. Above 45 HRC C45 leaves carbide behind and wants ceramic or CBN, which is usually the point at which grinding becomes the cheaper option.
Past 25 mm, the carbon steel stops being high strength and starts being a case
Use C45 for Load-bearing parts and the single most expensive mistake is specifying it on a section too thick to harden. Water quenching gives a critical diameter of about 20–25 mm for a 50% martensite core. A 60 mm shaft quenched in water has a hard skin and a soft centre, and the fatigue life you designed for belongs to the skin only.
That is the boundary where Alloy steel earns its price. Adding chromium and molybdenum — 42CrMo4 in EN, 4140 in AISI, SCM440 in JIS — pushes the through-hardening diameter from about 20 mm to somewhere between 50 and 75 mm, lifts the quenched and tempered strength to 900–1100 MPa, and improves toughness at the same hardness. The bar costs roughly 1.5 times as much as C45 and welds less willingly, which is exactly the trade you are making.
Mechanical structures and Load-bearing parts, in carbon and alloy steel
Mechanical structures and Load-bearing parts are what this page is for: the frames, plates, brackets, housings and shafts that hold a machine together and take the force. With Alloy steel kept in reserve for the sections that need it, three groups cover almost every drawing that arrives.
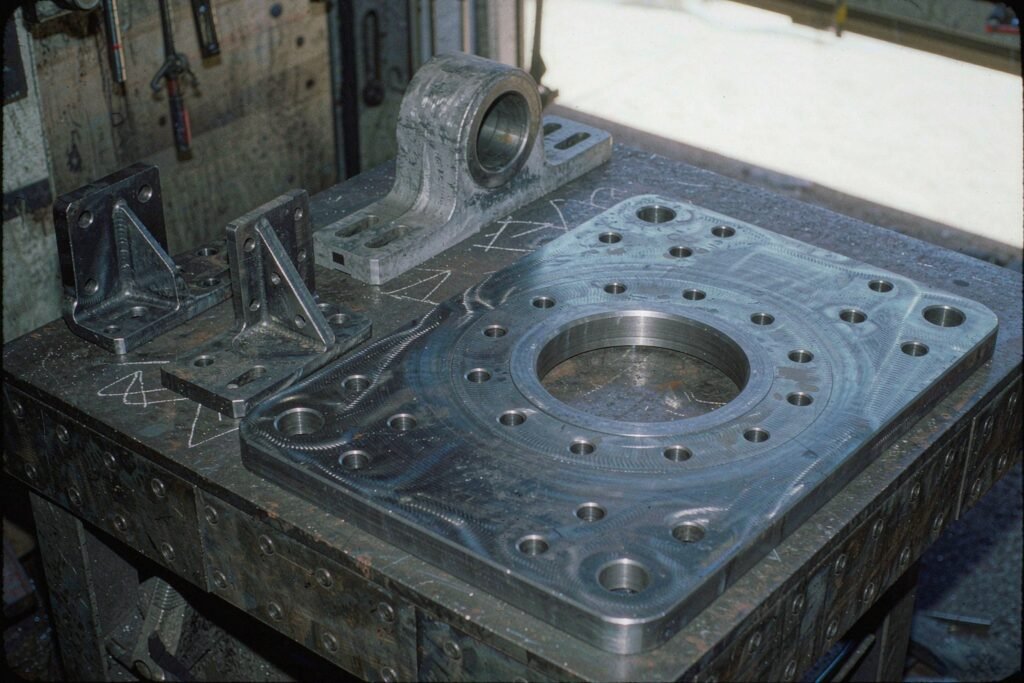

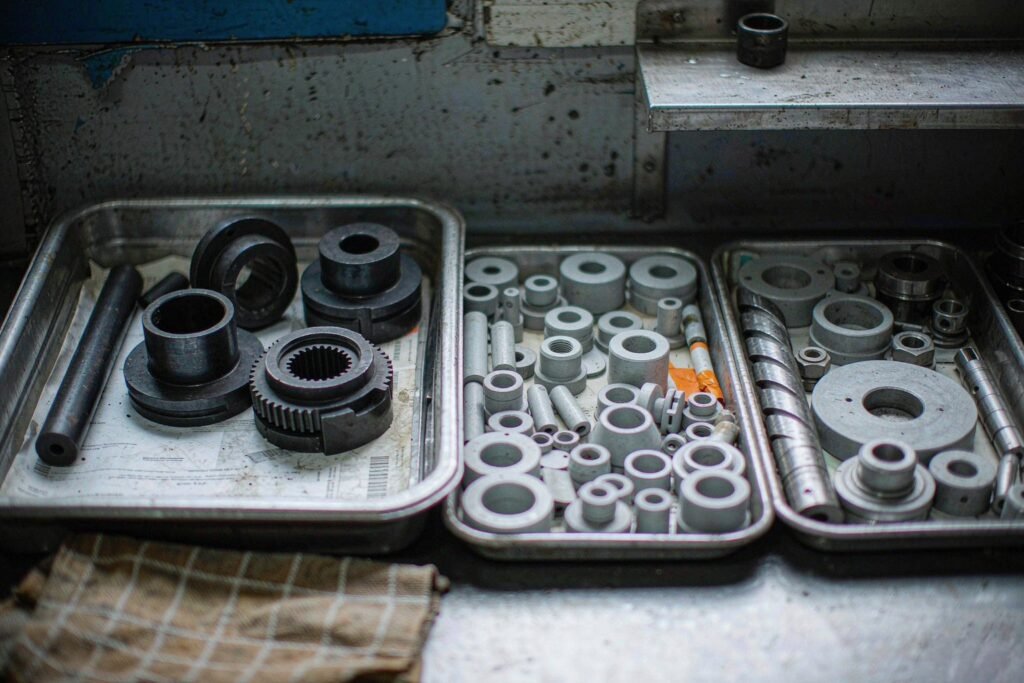
Four features cause most fatigue failures in steel shafts
Rotating parts fail from fatigue, not from being overloaded once. The bending stress reverses every revolution, the crack starts at the surface, and it starts wherever the geometry interrupts the load path. The stress concentration factor Kt tells you how much worse than nominal the local stress is. The circle on each card is drawn to scale against that number. These four features account for most of the fatigue failures XS Precision sees on returned steel shafts.
Machined C45 shafts: shoulder fillets, milled keyways and centre-drilled ends — the three features that decide fatigue life
The route matters more than the temperature on the ticket
A heat treatment specification that names only a hardness number leaves the shop to invent the sequence, and the sequence is what determines whether the part comes out on size. Quenching does three things at once: it sets the structure, it sets the residual stress, and it moves the geometry. Only the first of those is on the drawing.
Why the shaft was straight on the lathe and is not straight now
Machining removes material and redistributes internal stress; heat treatment changes the structure of what is left. A slender shaft can come out of the quench with 0.1–0.3 mm of bow per metre, and a part with shoulders, keyways and uneven section thickness will move more than a plain cylinder because it does not heat and cool evenly.
The answer is not to try to quench it straight. It is to plan the distortion: leave grinding stock on the controlled diameters, specify the straightness requirement against a stated datum and a stated length, and put straightening between hardening and final grinding where it can be measured and proved. Cold straightening of hardened steel is limited — past roughly 0.020 inch per foot of bow the part is more likely to fracture than to come back — and it has to be done below the tempering temperature or the martensite is locally re-tempered.

Heat treatment of C45 parts at the quench: structure, residual stress and geometry are all set in the same operation
Quench cracking, soft cores and a certificate that does not travel
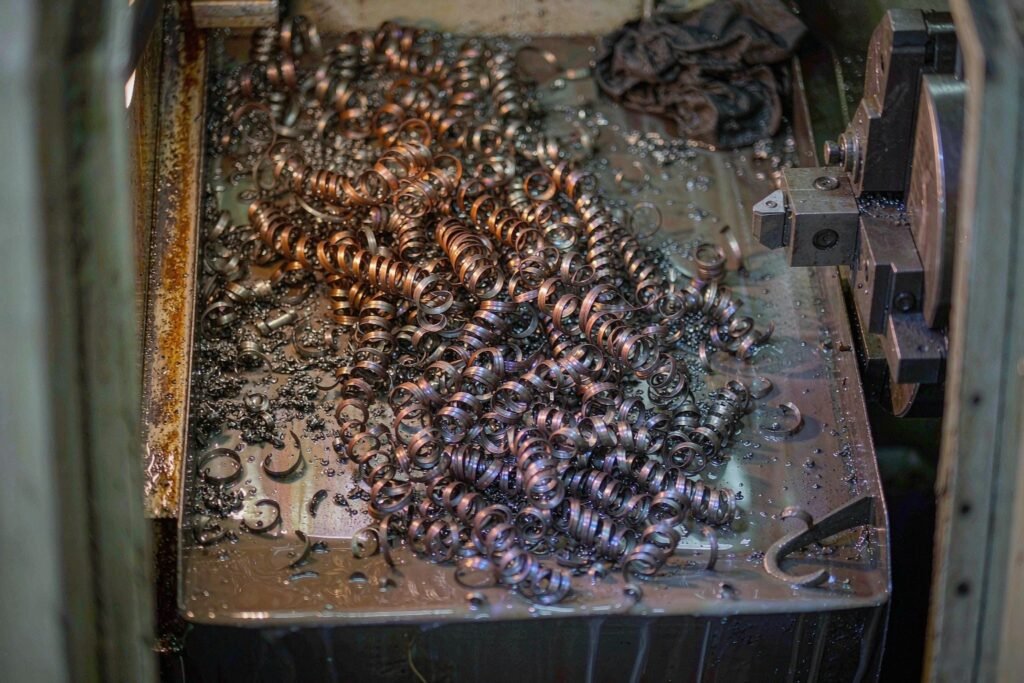
The swarth from turning C45: long continuous chips with temper colours from straw to blue, the same colours the temper scale above is drawn from
Carbon steel has no corrosion resistance, so the finish is a specification
Carbon steel and Alloy steel are both structural materials, not corrosion materials. Left bare in a damp workshop or a coastal installation, C45 will rust, and a rusted bearing seat is a tolerance that no longer exists. Every drawing that leaves the shop needs either a finish on it or a stated reason why it can be left bare.
The finishes differ mainly in what they do to the dimension. Black oxide builds a conversion layer of 1–2 µm and changes nothing — it is the default for tooling, fasteners and parts that are already at final size, and it carries no hydrogen embrittlement risk. Hard chrome builds 10–30 µm of 800–1000 HV material and is what keeps a hydraulic rod from wearing out, but high-strength steel must be baked at 190–220 °C for at least four hours after plating to drive out the hydrogen. Nitriding changes no dimension of consequence either, at the cost of a matte grey surface that cannot be machined afterwards.
Black oxide, nitrided and untreated machined steel parts, compared side by side
Cost-effective does not mean the cheapest bar per kilogram
Hot-rolled 45# round bar out of a Chinese mill was trading around US$550–680 per tonne FOB through 2026, with C45E carrying a 5–8% premium for the tighter phosphorus limit and the guaranteed impact test. US-produced 1045 sits at US$850–1,100 per tonne and 42CrMo4 at roughly US$750–760.
Those numbers are real and they are also only part of the story. On a finished machined part, the bar is usually less than half the cost. The rest is cutting time, tool life, fixturing and inspection — which is why a material with a 55–60 machinability index and a predictable heat treatment is often cheaper than a cheaper bar that machines badly or moves in the furnace. Reading a quote means reading the process, not just the material line.
One lever that drawings forget: bar diameter. C45 is stocked in a wide range of sizes, so choosing a nominal diameter that matches the stock rather than forcing a special size removes roughing time and swarf from the job before it starts. XS Precision runs that comparison at the quotation stage rather than after the first article.
Certificates, traceability and the check that is worth the money
EN 10204 defines four inspection document types, and the difference between them is who did the testing and whether the paperwork can be tied to the piece in your hand. Naming the type on the purchase order rather than asking for a general material certificate is the difference between documentary comfort and traceability.
A 3.1 certificate is worth exactly as much as its link to the delivered part. The heat number on the certificate has to match the stamp on the bar, and the bar has to be the one the part was cut from. If those three do not line up, the lot is mixed and the honest answer is to sort it before shipment rather than to explain it afterwards.
Two checks catch most of what goes wrong. Positive material identification with a handheld analyser takes about thirty seconds per sample and catches the near-equivalent substitution that paperwork cannot. A hardness test on the finished part is the cheapest way to prove that the heat treatment named on the drawing actually happened, because a C45 part that should read 250 HB and reads 170 HB did not get quenched and tempered, whatever the route sheet says. XS Precision records the heat number against every part in the lot rather than against the shipment as a whole.
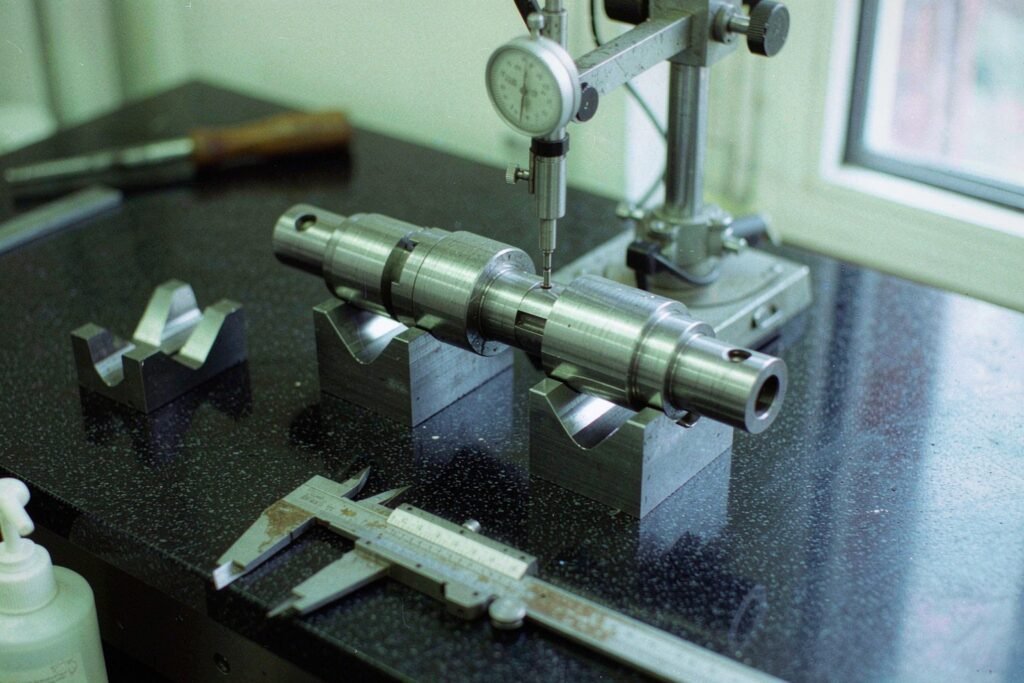
Dimensional inspection of a stepped steel shaft in V-blocks, with the heat number recorded against the part
Carbon Steel or Alloy steel: the questions that decide it
Four questions settle most of these decisions before the drawing goes out. Answer them in order and the grade usually chooses itself.
| IF THE PART… | THEN |
|---|---|
| Loads a section under 25 mm and needs strength after heat treatment | C45 quenched and tempered. You will get 700–850 MPa and a core that actually hardened. |
| Loads a section over 25 mm | Move to 42CrMo4. C45 will only harden the skin, and you will be paying for strength the core does not have. |
| Needs a hard surface on a finished size | Nitride a 42CrMo4 part at 500–550 °C, or induction harden C45 before the final grind where the geometry allows it. |
| Sees shock or impact at high strength | Either C45E with its guaranteed impact energy, or a nickel-bearing Alloy steel such as 40CrNiMoA if the section is also large. |
| Has to be welded | Weld before hardening, preheat 200–300 °C, use low-hydrogen consumables and stress relieve afterwards. If welding is central, a low-carbon steel is the better structural answer. |
| Faces chlorides or a wet environment | Neither grade is a corrosion material. Specify a coating, or move the part to stainless steel and accept the machining cost. |
What we would change before the drawing is released
Carbon steel and alloy steel questions, answered before the quote
Is C45 the same as 1045 and S45C?
For practical purposes, yes. C45 (EN 1.0503) has a carbon window of 0.42–0.50% with manganese 0.50–0.80%; AISI/SAE 1045 is 0.43–0.50% with manganese 0.60–0.90%; JIS S45C sits in the same band with a higher manganese ceiling and tighter impurity control. Mills routinely dual- or triple-certify one heat to all three. C45E is the cleaner European version, with phosphorus held to 0.030% instead of 0.045% and a guaranteed impact value.
Why did my shafts come back bent after heat treatment?
Because the material moved, which is normal, and because the route had nowhere to correct it. Slender shafts commonly bow 0.1–0.3 mm per metre through a quench, and parts with shoulders, keyways or uneven section thickness move more than a plain cylinder. The controlled answer is to leave grinding stock on the critical diameters, harden, measure against a stated datum, straighten cold and below the tempering temperature if needed, then grind to size. Finishing every journal before hardening and hoping is the one route that has no way back.
When should I stop using C45 and move to 42CrMo4?
When the load-bearing section is thicker than roughly 25 mm. That is the practical limit of C45’s hardenability in water — below it the part harden through, above it you get a hard case and a soft core. Chromium and molybdenum in 42CrMo4 push the through-hardening diameter to 50–75 mm and lift the quenched and tempered strength to 900–1,100 MPa. You pay about 1.5 times the bar price, a little machinability and a lot more care when welding.
Can you hold tight tolerances on a part that gets hardened?
Yes, by taking the tolerance off the hardened condition. Finish features to ±0.01 mm after heat treatment with light carbide cuts, or grind them, and leave 0.25–0.40 mm of stock on those surfaces through the furnace. Above 45 HRC, expect the realistic capability to open up to ±0.02–0.05 mm and grinding to become the cheaper route. What does not work is specifying a tight tolerance on a feature that is already at final size before quenching.
What surface finish should I specify on carbon steel?
Something, unless there is a stated reason not to. Black oxide is the default where the part is already at final size because it builds 1–2 µm and changes nothing. Hard chrome gives 800–1000 HV and 10–30 µm of wear-resistant material on rod and pin surfaces, with a 190–220 °C bake afterwards to remove hydrogen. Nitriding reaches 600–800 HV with minimal distortion but leaves a matte grey surface that cannot be machined, so it has to be the last operation. XS Precision will name the finish and the thickness on the quotation so the dimension stack can be checked before the parts are cut.
Do you supply material certificates, and can I see the heat numbers?
Yes. Every order ships with an EN 10204 3.1 inspection certificate carrying the heat number, with that number matched to the stamp on the bar the parts were cut from, plus a dimensional report at a stated measurement temperature. Positive material identification and hardness verification on finished parts can be added to the route where the application justifies them. If your end user requires 3.2 with independent third-party verification, say so at the RFQ stage rather than at shipment.
Related capability and material pages to read next
Precision CNC machining
Turning, milling and drilling on carbon and alloy steel, with the speeds, tooling and heat treatment sequence described above.
High-precision components
Bores, threads and ground journals held on hardened steel, with the dimensional report to match.
Brass and copper against steel
The other side of the same decision — where conductivity and machinability beat strength and cost.
Send the drawing. We will tell you which grade fits.
A STEP file, the section thickness at the load-bearing features and the service environment are enough to start. If the section is too thick for C45, or if a coating is the wrong answer for the environment, you will hear that before the quote rather than after the parts arrive.
Or send the drawing to info@xsprecisiontech.com with the grade, the delivery condition and the quantity, and we will come back with the machining route, the heat treatment sequence, the tolerance we can hold and the certificate package.