
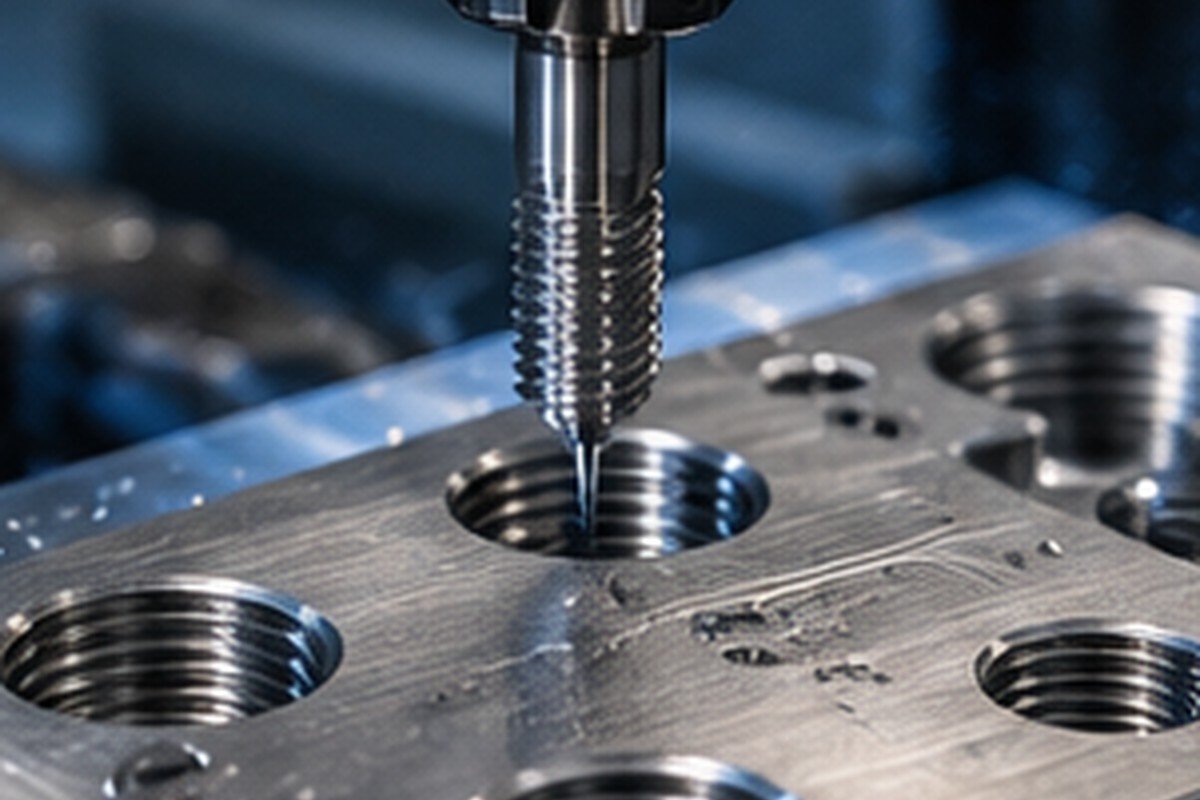
A threaded hole can look fine on a drawing and still create an assembly problem. The issue is often not thread size but the direction of the thread axis.
Thread alignment starts before tapping
The location and orientation of the pilot hole establish the starting condition for a thread. Check datum selection, workholding and spindle alignment before discussing a tapping cycle. A well-formed thread can still point in the wrong direction if the setup is incorrect.
Why a thread gauge is not a perpendicularity test
A go/no-go plug gauge primarily checks functional thread size. It cannot, by itself, demonstrate that the thread axis is square to a specified face. When angular alignment is critical, agree on an inspection method and reference datum before production.
Machining the thread in the primary setup
Keeping drilling and tapping in a controlled CNC setup can reduce repositioning risk. Separate tapping equipment may be appropriate for some work, but it introduces another setup and requires process validation. The best route depends on the drawing, access and volume.
What to specify on an RFQ
Provide thread standard, nominal size, pitch, depth, through or blind condition, datum and any perpendicularity requirement. Clarify whether thread inserts, thread milling or tapping are permitted. For critical joints, ask how alignment will be verified.
A practical inspection conversation
Ask for the actual measurement approach rather than a general promise of 100% inspection. A calibrated indicator setup, a suitable threaded alignment gauge or a CMM-based method may be relevant depending on tolerance and geometry. Each method has limits that should be understood.
Additional manufacturing considerations
A thread can pass inspection and still be wrong
A GO/NO-GO thread gauge answers an important question: will the specified thread engage within its size limits? It does not establish whether the thread axis is perpendicular to a mounting face. That distinction matters when a screw clamps a cover, locates an assembly or mates with a rigid component. A part can accept the gauge while the fastener visibly leans when installed.
The drilled hole may be out of position or angle before tapping begins. A separate tapping operation adds another setup and another opportunity for misalignment. Tool deflection, poor chip evacuation and unstable workholding can also contribute. Moving tapping into a CNC setup can reduce handling, but it is not a guarantee: the machine, toolholder, hole preparation and datum strategy still matter.
Choose a control plan around the function
Start with the drawing: which face is the functional datum, and what angular or positional relationship must the threaded feature satisfy? If assembly alignment is critical, define a measurable requirement rather than relying on a vague note such as “thread straight.” Depending on geometry, inspection may use a qualified threaded inspection pin with a perpendicularity fixture, a CMM strategy, or a functional assembly gauge. Agree on the method before production.
Provide the thread specification, depth, blind or through condition, datum references and the mating-part function. For blind holes, identify usable full-thread depth separately from drill depth. If the drawing requires 100% inspection, specify that at quotation stage; it changes inspection time and may require a dedicated gauge.
Ask how the supplier controls the hole and thread axis relative to the mounting datum, not merely whether they own thread plug gauges. A credible answer should describe setup, toolpath and verification. The same principle applies to other features: inspection should measure the requirement that actually affects assembly.
Ask the supplier to identify the drawing revision being quoted, any assumptions that affect cost, and the inspection evidence that will accompany the parts. Where a feature is critical to assembly, agree on a measurable acceptance method before production begins.
If you are sourcing custom CNC machined components, send XS Precision your 2D drawing, 3D model, material specification, quantity and required inspection documents. We can review the manufacturing scope and clarify open technical questions before preparing a quotation.
Questions to resolve before placing an order
- Which dimensions or functional interfaces are critical for this CNC threaded holes project?
- What material, finish and inspection evidence should be included with each shipment?
- Which drawing revision, quantity and delivery assumptions should the supplier use?
Discuss your part with XS Precision
If you are sourcing custom CNC machined components, send XS Precision your 2D drawing, STEP model, material specification, quantity and inspection requirements. We can review the manufacturing requirements and prepare a quotation based on the information provided.
Website: https://xsprecisiontech.com/